arrow icon Back

Remote Control Bentonite Pumping Boosts Productivity on the A9

  • Background

    Our customer is a civil engineering and horizontal directional drilling contractor based in the North East of Scotland. The business delivers high-quality solutions for homeowners, businesses and large-scale infrastructure projects across Aberdeen, Aberdeenshire and beyond.

    For this project, the team worked on the A9 at Ballinluig in Perthshire. As with every job, their aim was to work efficiently, keep costs under control and reduce their environmental impact, all while delivering to a tight budget.
  • The Challenge

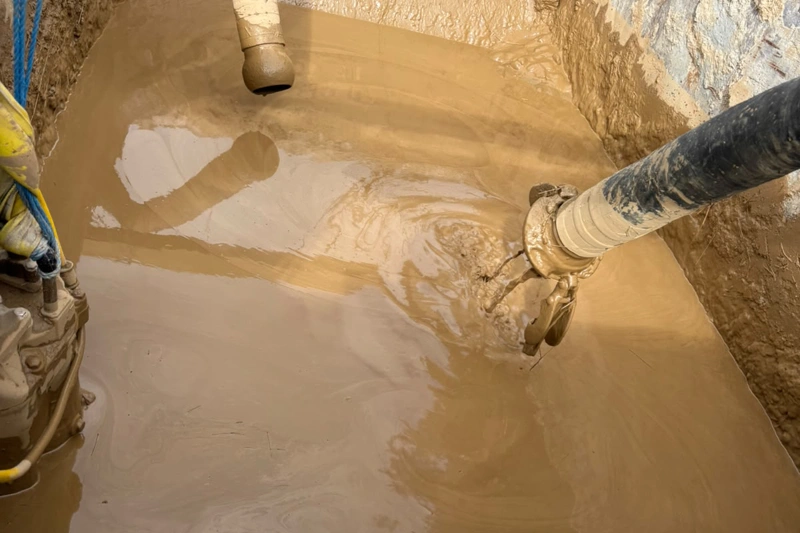
    Horizontal directional drilling relies on a constant, well-managed supply of bentonite. However, the existing pump setup meant it could only be switched on and off by hand, at the pump itself.

    This left the customer with two inefficient options:

    • With just one operator on site, he had to climb out of the drilling rig every time the pump needed starting or stopping
    • With two people on site, one had to stand by the pump all day just to operate it while the other ran the rig

    Either way, the business was losing time, money and productivity on a project where every hour counted.

  • The Solution

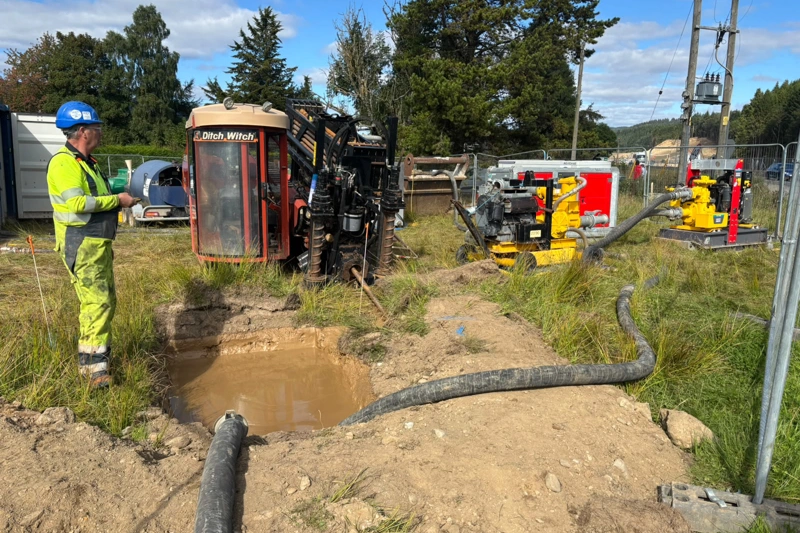
    The customer brought the problem to GAP, and the Pump Services division came back quickly with a practical answer: a 4” diesel bentonite pump fitted with a remote control.

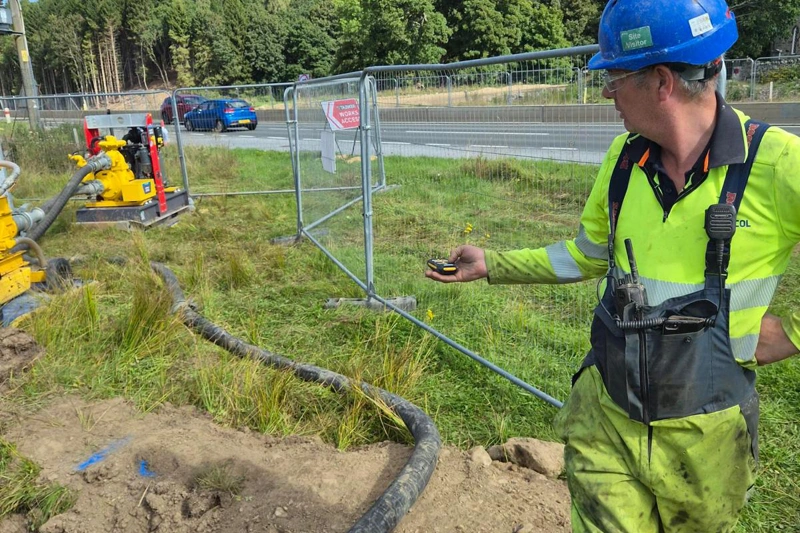
    The rig operator can now start and stop the pump from the cab, so there’s no need to leave the rig or to keep a second person on the pump.

  • Products & Services Used

    • Atlas Copco PAS 100MF 4” diesel vacuum-assisted self-priming pump with a Stage V engine
    • Remote control unit for start/stop operation from the drilling rig
  • The Result

    Adding remote control to the bentonite pump brought clear benefits on site:

    • Time saved: the operator stays at the controls instead of repeatedly leaving the rig
    • Cost savings: a second person no longer needs to be on site just to run the pump
    • Higher productivity: drilling carriers on with fewer interruptions
    • Lower emissions: the pump runs only when it’s needed, which cuts unnecessary running time

    The results were so strong that the customer has since ordered more of there pumps for future work.

  • The Experience

    The customer described working with GAP as “Excellent” and said what stood out most was how quickly the solution was provided.

    The customer commented, “GAP has been fantastic. We gave them an issue, and they provided us with a solution. The GAP pump is now the first choice, and the competitor pump is now the backup choice.”

  • Conclusion

    The A9 project shows how a simple, well-chosen change can make a real difference on site. By pairing a reliable bentonite pump with remote control, GAP’s Pump Services division helped the customer save time, cut costs and reduce emissions. It has also earned GAP a place as the customer’s first-choice pump supplier.

    To find out how GAP’s Pump Services division can support your next project, contact your local GAP depot.